Cost and Lead Times for Industrial Powder Coating Lines
Powder coating equipment costs and lead times vary significantly based on line capacity, automation, and current supply chain conditions. This guide breaks down capital expenditure factors and installation timelines to help buyers plan realistic budgets and project schedules for new facilities.
- Total line costs are driven by capacity, automation level, and material handling systems, not just the oven or booth.
- Supply chain delays often affect critical components like controllers, motors, and specialized filtration systems.
- A clear RFQ with detailed specifications allows vendors to provide comparable quotes and realistic lead times.
- Installation timelines typically exceed equipment manufacturing time due to site preparation and utility connections.
- Comparing quotes requires a standardized format to evaluate total cost of ownership, not just the equipment price.
What Drives the Price of a Powder Coating Line
The cost of powder coating equipment is rarely a single line item. A complete facility investment includes the application booth, the curing oven, the filtration system, the powder delivery unit, and the control panel. Each component has a different cost structure, and the final price depends on how they are integrated.
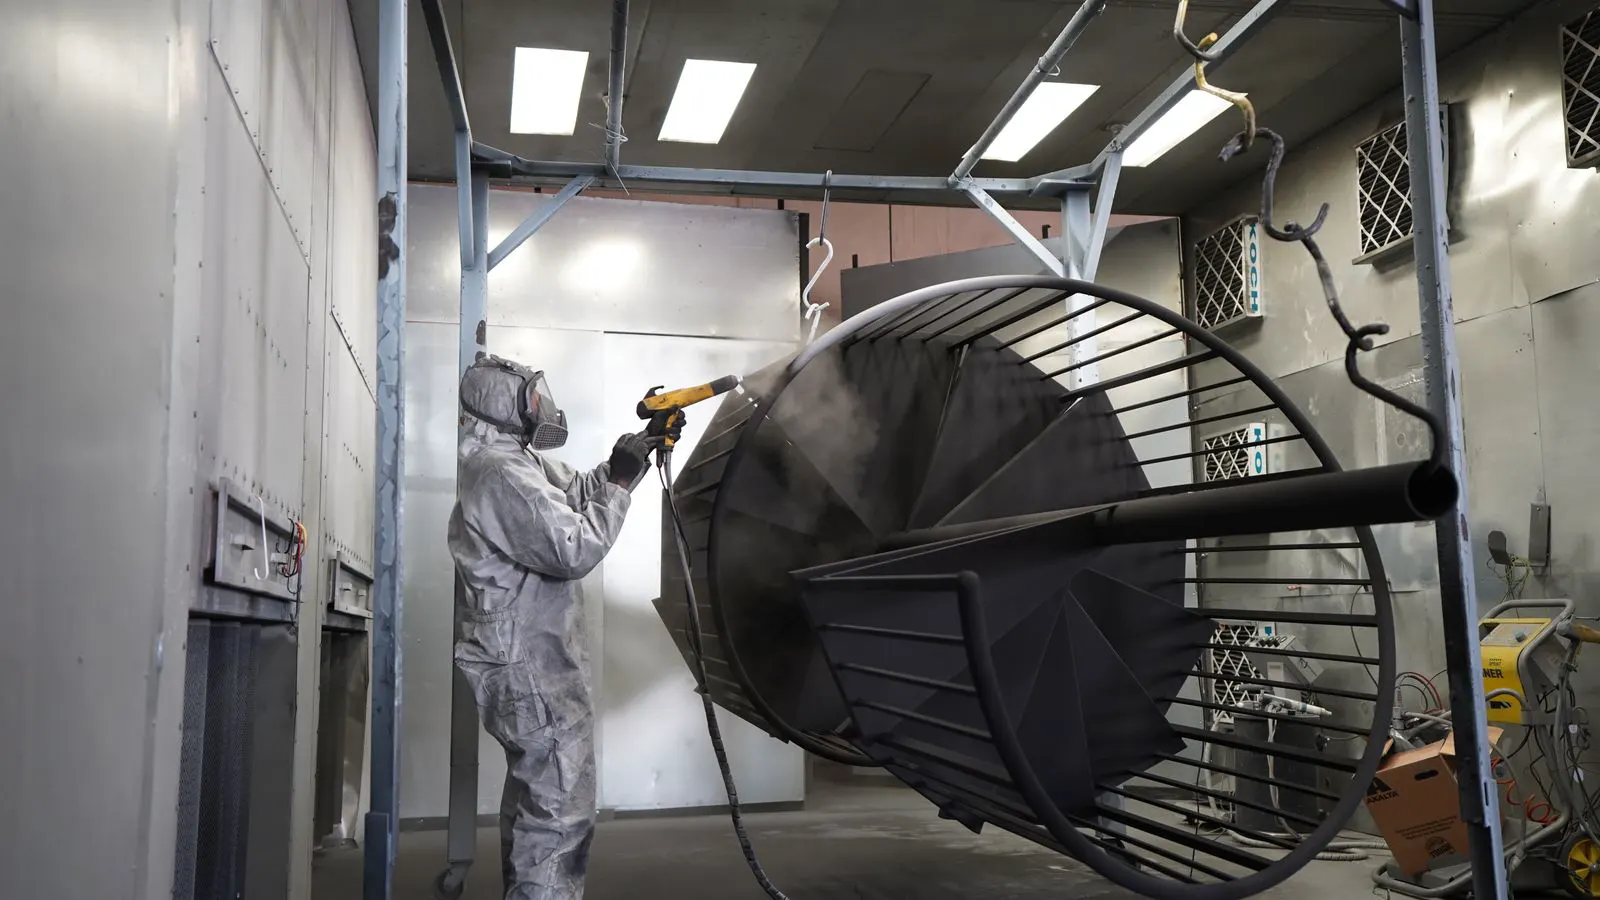
Application booths range from simple open-frame designs to enclosed spray booths with high-efficiency filtration. Enclosed booths cost more but reduce overspray and improve environmental compliance. The filtration system, often a baghouse or filter wheel, scales with the booth volume. A larger booth needs a bigger filtration unit to maintain airflow. If the booth handles a high volume of parts, the filtration system must also handle more particulate load, which increases the size of the filter wheels and the frequency of maintenance. A poorly sized filtration system can clog quickly, leading to pressure drops and reduced capture efficiency. This forces operators to stop the line for cleaning, which stops production.
The curing oven is another major cost driver. Conventional ovens run on natural gas or electricity, while infrared ovens offer faster cure times at higher energy costs. The size of the oven matches the conveyor width and the maximum part size. Larger ovens require thicker insulation and larger burners, which increases the capital expenditure. The choice of fuel also affects the installation requirements. A natural gas oven needs a gas train, pressure regulators, and safety interlocks that a purely electric oven does not. If the facility already has a gas line, the installation cost is lower. If it does not, the cost of extending the line or installing a new metering station adds to the project budget.
The powder delivery system includes the powder hopper, the electrostatic gun, and the powder recirculation unit. For high-volume lines, a central powder system with multiple guns is more expensive but reduces labor. The central system uses a larger hopper and a pneumatic transfer system to supply powder to multiple guns simultaneously. This setup is ideal for lines with many stations or where different parts require different colors. The point-of-use system is cheaper and simpler, but it requires more frequent refilling and changes color more slowly. The control panel ties everything together. A basic panel monitors temperature and conveyor speed. A programmable logic controller panel adds recipe storage, data logging, and remote monitoring. A PLC panel allows operators to save specific cure profiles for different products. This is particularly useful in mixed-production environments where the oven must cure aluminum, steel, or plastic parts with different temperature requirements. The data logging feature provides a record of every cycle, which is useful for quality audits and process control.
How Supply Chain Delays Affect Lead Times
Lead times for powder coating equipment depend on the availability of standard components and the complexity of the custom engineering. Standard parts like motors, pumps, and basic electrical components usually have shorter lead times. Custom parts like specialized oven doors, custom conveyor frames, or integrated control panels take longer to manufacture. The complexity of the custom engineering often determines the longest lead time in the project. For example, an oven with a non-standard door height or a conveyor with a specific turn radius may require custom fabrication. These parts must be designed, approved, and manufactured before the assembly phase can begin.
The current supply chain environment affects every stage of production. Raw materials for steel structures and insulation can have variable lead times. Electronic components for control panels may experience delays. If a vendor sources parts from multiple suppliers, the longest lead time determines when the complete unit can be shipped. This is a common source of project delays. A vendor may have the booth and oven ready, but if the control panel is waiting on a specific type of relay or touch screen, the whole system cannot be shipped. The buyer is left waiting while the vendor coordinates with the electronics supplier.
Buyers should ask vendors for a breakdown of lead time by component. A vendor might quote twelve weeks for the booth and eight weeks for the oven, but if the control panel takes sixteen weeks, the whole line ships in sixteen weeks. This information helps buyers understand where delays are most likely to occur. It also helps in planning the installation schedule. If the control panel is the long pole, the site preparation can be completed early, but the electrical connection for the panel should be reserved. This prevents the site team from having to wait while the panel is being manufactured.
How to Write a Clear RFQ
A Request for Quote that lacks detail leads to vague answers and wide price ranges. A clear RFQ states the exact application, part dimensions, and production volume. It lists the required finish types, such as standard polyester or high-solids powder. It specifies the cure temperature and the required coating thickness. The RFQ should also mention the substrate. For example, a line coating galvanized steel behaves differently from a line coating raw steel or aluminum. The substrate affects the pre-treatment requirements and the adhesion of the powder.
The RFQ should include the facility layout. A 2D drawing of the floor space helps vendors design the conveyor path and oven placement. It should list the utility connections available, such as compressed air pressure, electrical service, and exhaust venting. If the facility has existing environmental controls, those details should be included. The RFQ should also state the maximum part size and weight. A part that is 2 meters long and 500 kg requires a different conveyor and oven structure than a part that is 30 cm long and 2 kg. The weight affects the conveyor load rating and the oven door size.
State the expected production rate. For example, a line that processes 500 parts per hour needs different equipment than a line that processes 50 parts per hour. The RFQ should also ask for the estimated lead time and the payment terms. Some vendors offer staged payments tied to milestones, which can affect cash flow. For instance, a payment structure might require 30 percent at order confirmation, 40 percent at factory acceptance testing, and 30 percent at delivery. This structure aligns the vendor’s cash flow with the project progress and reduces the buyer’s risk if the project is delayed.
How to Compare Quotes Fairly
Vendors often price different items separately. One quote may include the booth but not the powder delivery system. Another may include the oven but not the control panel. To compare quotes fairly, create a standardized comparison sheet. List each major component and check if it is included in the price. This sheet should include the booth, the filtration system, the oven, the conveyor, the powder system, the control panel, and any auxiliary equipment such as pre-treatment tanks or drying racks.
Look at the total cost of ownership, not just the purchase price. A cheaper line with higher energy consumption or higher maintenance costs may be more expensive over time. Ask about the expected lifespan of key components. Ask about the warranty terms and what is covered. Ask about the availability of spare parts and technical support. For example, a vendor that provides spare filters and a technical support line with a guaranteed response time may be more valuable than a vendor with a slightly lower purchase price but a long wait time for spare parts.
Also compare the installation scope. Some vendors provide the equipment only. Others provide installation, commissioning, and operator training. The installation cost varies based on the site conditions. A vendor that includes installation in the quote may have a higher initial price but a lower total cost than a vendor that sells the equipment only. The installation team knows how the equipment works and can identify issues during commissioning. This can prevent problems that would otherwise be discovered after the line is in production.
Installation Timeline and Site Requirements
The installation timeline starts after the equipment arrives. Site preparation is the first phase. The floor must be level and reinforced to support the weight of the oven and conveyor. Electrical panels need to be installed and connected. The exhaust system must be vented to the outside. The level of the floor is critical. If the floor is not level, the conveyor may bind, and the oven doors may not close properly. This requires additional floor grinding or the installation of adjustable feet, which adds cost and time.
The equipment is delivered in modules or as a single unit. The booth and oven are often bolted to the floor. The conveyor is assembled on site. The powder system is connected to the powder hopper and the guns. The control panel is programmed and tested. The connection of the powder system requires a clean and dry environment. If the site is dusty, the powder may clump in the lines, causing blockages. This requires flushing the system with air or cleaning the lines before the first production run.
Commissioning takes several days. The team runs the line with water or test powder to check for leaks, airflow issues, and temperature accuracy. They adjust the conveyor speed and the oven zones. They train the operators on daily checks and troubleshooting. The total installation time depends on the complexity of the line and the readiness of the site. A site that is ready with all utilities connected and the floor prepared will have a shorter installation time. A site that requires additional civil work or electrical upgrades will have a longer installation time.
Cost Drivers at a Glance
The following table lists the main cost drivers for a new powder coating facility. The relative weight of each driver varies by project.
| Cost Driver | Description | Typical Impact |
|---|---|---|
| Application Booth | Size, filtration level, and enclosure type | High |
| Curing Oven | Fuel type, size, and energy efficiency | High |
| Powder Delivery | Central vs. point of use, number of guns | Medium |
| Control System | PLC complexity, data logging, remote access | Medium |
| Site Preparation | Floor work, electrical, exhaust, and permits | Variable |
| Installation | Labor, commissioning, and training | Medium |
Planning for Budget and Schedule Risk
Budgets for capital expenditure projects should include a contingency. Supply chain delays and site issues can push costs higher than the initial estimate. A 10 to 15 percent contingency covers unexpected material price changes and minor design changes. This contingency should be kept separate from the base budget. It is not for adding new features or increasing the production rate. It is for covering the risks that are inherent in the project. For example, if the steel price rises during the manufacturing phase, the contingency can cover the difference. If the site requires additional electrical work, the contingency can cover the extra labor and materials.
The schedule should also include buffer time. If the vendor quotes twelve weeks for manufacturing, plan for sixteen weeks to account for shipping delays and site readiness. If the site is not ready when the equipment arrives, the installation clock stops. This can extend the project by several weeks. To avoid this, the buyer should align the equipment delivery with the site readiness. This requires close coordination between the equipment vendor and the site contractor. The buyer should be the point of contact for both parties.
Buyers should maintain a single point of contact with the vendor. This person should manage the design review, the production status, and the installation planning. Regular communication reduces the risk of miscommunication and helps identify issues early. For example, if the vendor discovers a problem with a part during manufacturing, the single point of contact can discuss the solution with the buyer. This prevents the problem from being discovered during installation, which would cause a delay.
The goal is a facility that meets the production requirements and operates within the planned budget and schedule.
Frequently asked questions
What is the most expensive component of a powder coating line?
The curing oven and the application booth with high-efficiency filtration are typically the largest cost items. The control system and powder delivery also add to the total.
How long does it take to install a standard powder coating line?
Installation usually takes one to three weeks, depending on the complexity of the site and the equipment. Commissioning and training add a few more days.
Can I buy the equipment separately from the installation?
Yes, some vendors sell the equipment without installation. Others offer a turnkey package. Buying separately may save money if you have in-house installation expertise.
What information do I need to provide for an accurate quote?
Provide part dimensions, production rate, finish types, cure temperature, and the facility layout. Include utility details like electrical service and compressed air.
How do supply chain delays affect my project timeline?
Delays in electronic components or custom parts can extend the manufacturing time. Ask the vendor for a component-level lead time breakdown to identify risks.