Fixing Low Coverage and Over-Spray in Industrial Coating
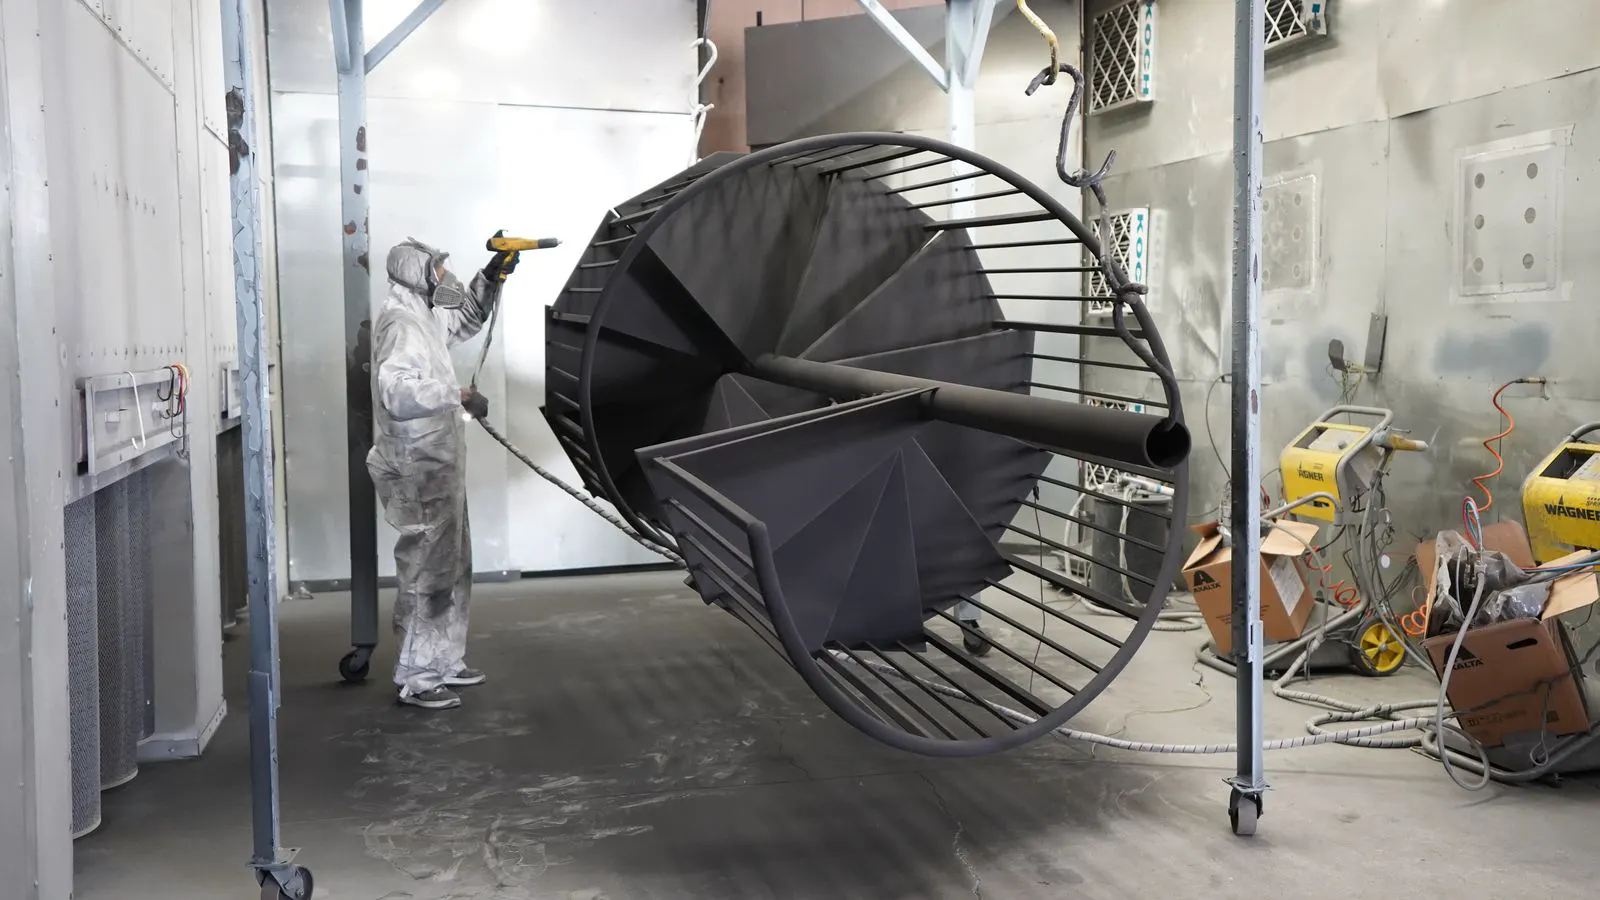
Low coverage and over-spray waste material and extend rework. This guide lists the most common symptoms, identifies likely causes such as wrong nozzle size, poor agitation, or incorrect film thickness, and provides actionable fixes to improve coverage and spray efficiency on production lines.
- Low coverage usually points to insufficient material delivery, incorrect nozzle selection, or poor surface preparation.
- Over-spray is often caused by high fluid pressure, incorrect fluid viscosity, or insufficient booth air movement.
- Fixing both issues requires matching the equipment to the product formulation and the specific surface being coated.
- Regular nozzle inspection and viscosity testing are the fastest ways to stop material waste.
- Documenting settings and material changes helps teams track performance and reduce rework on repeat jobs.
Why Coverage Falls Short in Industrial Coating
Coverage is the amount of material that actually stays on the substrate and builds the required film thickness. When coverage is low, the finish may appear patchy, show bare metal, or fail to pass a thickness check. The problem is rarely a single failure. It usually involves a combination of equipment settings, material handling, and process discipline.
A common early sign is that the spray pattern looks fine on a test card, but the production part still shows thin spots. This gap happens because the test card is flat and uniform, while the production part has edges, corners, and curved surfaces that pull material away from the target zone. If the equipment is not dialed in for the real part, the operator will keep spraying longer to compensate. That extra time creates over-spray, which then worsens the efficiency problem.
Understanding the cause matters because each cause has a different fix. A low-viscosity problem needs a viscosity adjustment. A nozzle problem needs a nozzle change. A booth problem needs air pattern correction. The table below lists the most common symptoms, the likely causes behind them, and the steps that usually resolve them.
| Symptom | Likely cause | What to do |
|---|---|---|
| Thin or patchy film on flat surfaces | Nozzle worn, clogged, or wrong size for the material | Replace or clean the nozzle, then verify the spray pattern on a test card at the working distance |
| Heavy over-spray at the edges of the part | Working distance too far or gun angle not perpendicular | Reduce working distance to the recommended range and keep the gun square to the panel |
| Low coverage on corners and edges | Material not building where the part geometry changes | Use a smaller tip or change the pattern shape to match the geometry, then adjust the travel speed |
| Drip or sag after the film cures | Fluid viscosity too low or application rate too high | Raise viscosity to the manufacturer range and reduce the overlap or slow the travel speed |
| Poor coverage on rough or textured surfaces | Surface not clean or not primed | Clean the surface and apply a suitable primer to level the substrate before the topcoat |
| Over-spray increasing over a shift | Booth air velocity dropping or filter load increasing | Check air velocity, clean or replace filters, and verify booth airflow pattern |
What Low Coverage Looks Like in Practice
Low coverage does not always look the same on every job. On a flat panel, it may show as a pale, uneven sheen. On a curved part, the thin spots often appear on the edges or in the shadow zones where the spray pattern does not reach. On a rough surface, the material may look present but the film thickness still fails because the substrate is consuming material in the pits and valleys.
The most reliable check is a thickness measurement, not visual inspection alone. A finish can look smooth but still be below the required thickness. A practical test is to measure at several points across the part, including the center and the edges. If the edge values are consistently lower, the problem is usually spray pattern or part geometry. If the center values are low, the problem is more often material delivery or nozzle condition.
Operators sometimes try to fix low coverage by simply spraying longer. That approach increases material use but rarely fixes the root cause. It usually creates a thicker film in the center, a thinner film at the edges, and a higher volume of over-spray. The result is a more expensive part, not a better one.
How Over-Spray Reduces Coverage and Efficiency
Over-spray is the material that leaves the gun and does not land on the part. It falls to the floor, sticks to the booth walls, or settles in the filters. Every drop of over-spray is a drop of material that did not contribute to the film. In a production environment, over-spray also creates a cleanup burden and can affect the booth air pattern.
A high over-spray rate can be caused by several factors. The fluid pressure may be too high, which atomizes the material into droplets that are too small to reach the part. The fluid viscosity may be too low, which makes the material easier to atomize but harder to control. The working distance may be too far, which scatters the pattern and reduces the density of material on the target. The booth air may be moving the mist away from the part before it lands.
Reducing over-spray is not the same as reducing coverage. A gun can have low over-spray and still produce a thin film if the material is not reaching the surface. The goal is to keep the material where it belongs. That means matching the gun settings to the material and the part, then checking the result with a test card and a thickness measurement.
Matching the Nozzle and Pattern to the Material
The nozzle is the point where the material leaves the gun. If the nozzle is wrong, the coverage will be wrong. A nozzle that is too large for the material produces a thick, uncontrolled pattern. A nozzle that is too small produces a fine mist that scatters easily. The pattern shape should match the part geometry. A round pattern works for flat panels. A fan or wider pattern works for edges and corners.
A practical way to choose the nozzle is to start with the material manufacturer’s recommendation, then adjust for the part. If the part has many edges, a wider pattern may be needed. If the part is large and flat, a narrower pattern may be more efficient. The working distance should be the distance where the spray pattern is fully formed and the droplets are still dense enough to land on the part. If the distance is too short, the pattern is concentrated and may drip. If it is too long, the pattern scatters and over-spray increases.
Nozzles wear over time. A worn nozzle produces an uneven spray and can cause low coverage even when the other settings are correct. Inspecting the nozzle is one of the fastest checks. A clean, sharp nozzle produces a symmetric pattern. A clogged or worn nozzle produces a broken or uneven pattern. Replacing the nozzle when it is worn is cheaper than reworking the part.
Controlling Viscosity and Material Delivery
Fluid viscosity is one of the most common causes of both low coverage and over-spray. If the fluid is too thin, it atomizes too easily and scatters. If it is too thick, it does not flow out of the nozzle evenly and can create a pattern with gaps. The material manufacturer provides a viscosity range. Staying inside that range is the baseline.
Viscosity can drift during a shift. Temperature changes affect the fluid. The material may also be affected by how it is mixed. A practical check is to measure viscosity at regular intervals, not just at the start of the shift. If the viscosity is outside the range, adjust the thinner or concentrate the material before continuing. This is especially important when the material is being used on a hot day or in a cold shop.
Material delivery also matters. A low fluid pressure can cause the material to break into a fine mist that does not reach the part. A high fluid pressure can cause the material to be thrown too far and to scatter. The fluid pressure should be set within the range recommended for the nozzle and the material. If the pressure is too high, the over-spray will increase. If it is too low, the coverage will fall short.
Checking the Booth and Air Movement
The booth is part of the coating system. It does not just hold the part. It moves the air that carries the mist to the part and removes the over-spray. If the booth air is not moving correctly, the material will not land where it is supposed to.
A common booth problem is insufficient air velocity. When the air is too slow, the mist does not get pulled toward the part. It falls to the floor or sticks to the booth walls. This increases over-spray and reduces coverage. Another common problem is a poor airflow pattern. The air may be moving too strongly in one direction, pushing the mist away from the part. In that case, the part may look fine in the center but thin at the edges.
A practical booth check is to measure the air velocity at the part location. The velocity should be within the range that keeps the mist on target without blowing it away. If the velocity is too high, reduce the fan speed or adjust the air pattern. If it is too low, increase the fan speed or clean the filters. The booth filters should also be checked. A loaded filter reduces airflow and changes the pattern.
Preventing Low Coverage and Over-Spray
Prevention starts with a consistent process. The same settings should be used for the same part and the same material. If the settings change, the result changes. A simple log of nozzle size, fluid pressure, viscosity, working distance, and booth air velocity makes it easier to spot problems before they become rework.
A test card is a useful tool. It should be sprayed at the start of each shift and after any change to the material or settings. The card should be checked for pattern shape, edge density, and thickness. If the card is good, the part is likely to be good. If the card is not good, the part will not be good.
The surface preparation step is also part of the coverage process. A clean, dry surface gives the material something to bond to. A dirty or oily surface can cause the material to bead or lift. A rough surface can consume material in the texture. In both cases, the film may be thin even if the spray pattern looks good.
Operator training matters as well. An operator who understands the cause and effect of each setting can make faster adjustments. A setting that works for one material may not work for another. A setting that works for a flat panel may not work for a complex part. The operator should know how to check the pattern, measure the thickness, and adjust the settings in a controlled way.
When to Escalate the Problem
Some low coverage problems are not fixed by small adjustments. If the material is not wetting the surface, the problem may be with the surface preparation or the material itself. If the nozzle is new and the settings are correct but the coverage is still low, the problem may be with the fluid pressure or the booth air. In those cases, the issue should be escalated to a process engineer or the supplier.
A supplier can help identify whether the material is being used outside its intended range. A process engineer can help check the equipment settings and the booth airflow. The goal is to find the root cause, not to keep compensating with more material. A small fix to the nozzle, the viscosity, or the booth air can save a lot of rework.
The same logic applies to over-spray. If the over-spray is high even after the nozzle, viscosity, and booth air are checked, the problem may be with the part geometry or the gun technique. In that case, the process may need to be changed. A different pattern, a slower travel speed, or a different working distance can reduce over-spray without reducing coverage.
The result of a well-managed process is a finish that passes the first check. The material is used where it belongs. The cost per part stays stable. The rework rate stays low. The booth stays cleaner. The operator spends less time on adjustments and more time on the actual coating work.
Frequently asked questions
What is the fastest way to check if low coverage is a nozzle problem?
Spray a test card at the normal working distance and inspect the pattern. A clean nozzle produces a symmetric, dense pattern. A worn or clogged nozzle produces a broken or uneven pattern.
How do I know if the fluid viscosity is too low for the material?
Measure the viscosity with a viscometer and compare it to the manufacturer range. If it is below the range, the material will atomize too easily and scatter. Raise the viscosity before continuing.
Can over-spray be fixed by changing the working distance only?
Changing the working distance can reduce over-spray, but it may not fix low coverage. If the over-spray is high, check the fluid pressure, viscosity, and booth air as well.
What is the best way to prevent low coverage on corners and edges?
Use a wider pattern or a smaller tip that matches the part geometry. Adjust the travel speed and overlap so the material builds where the part changes shape.
How often should the booth air velocity be checked?
Check it at the start of each shift and after any filter change or fan adjustment. A drop in velocity is often the first sign that the booth is not moving the mist correctly.